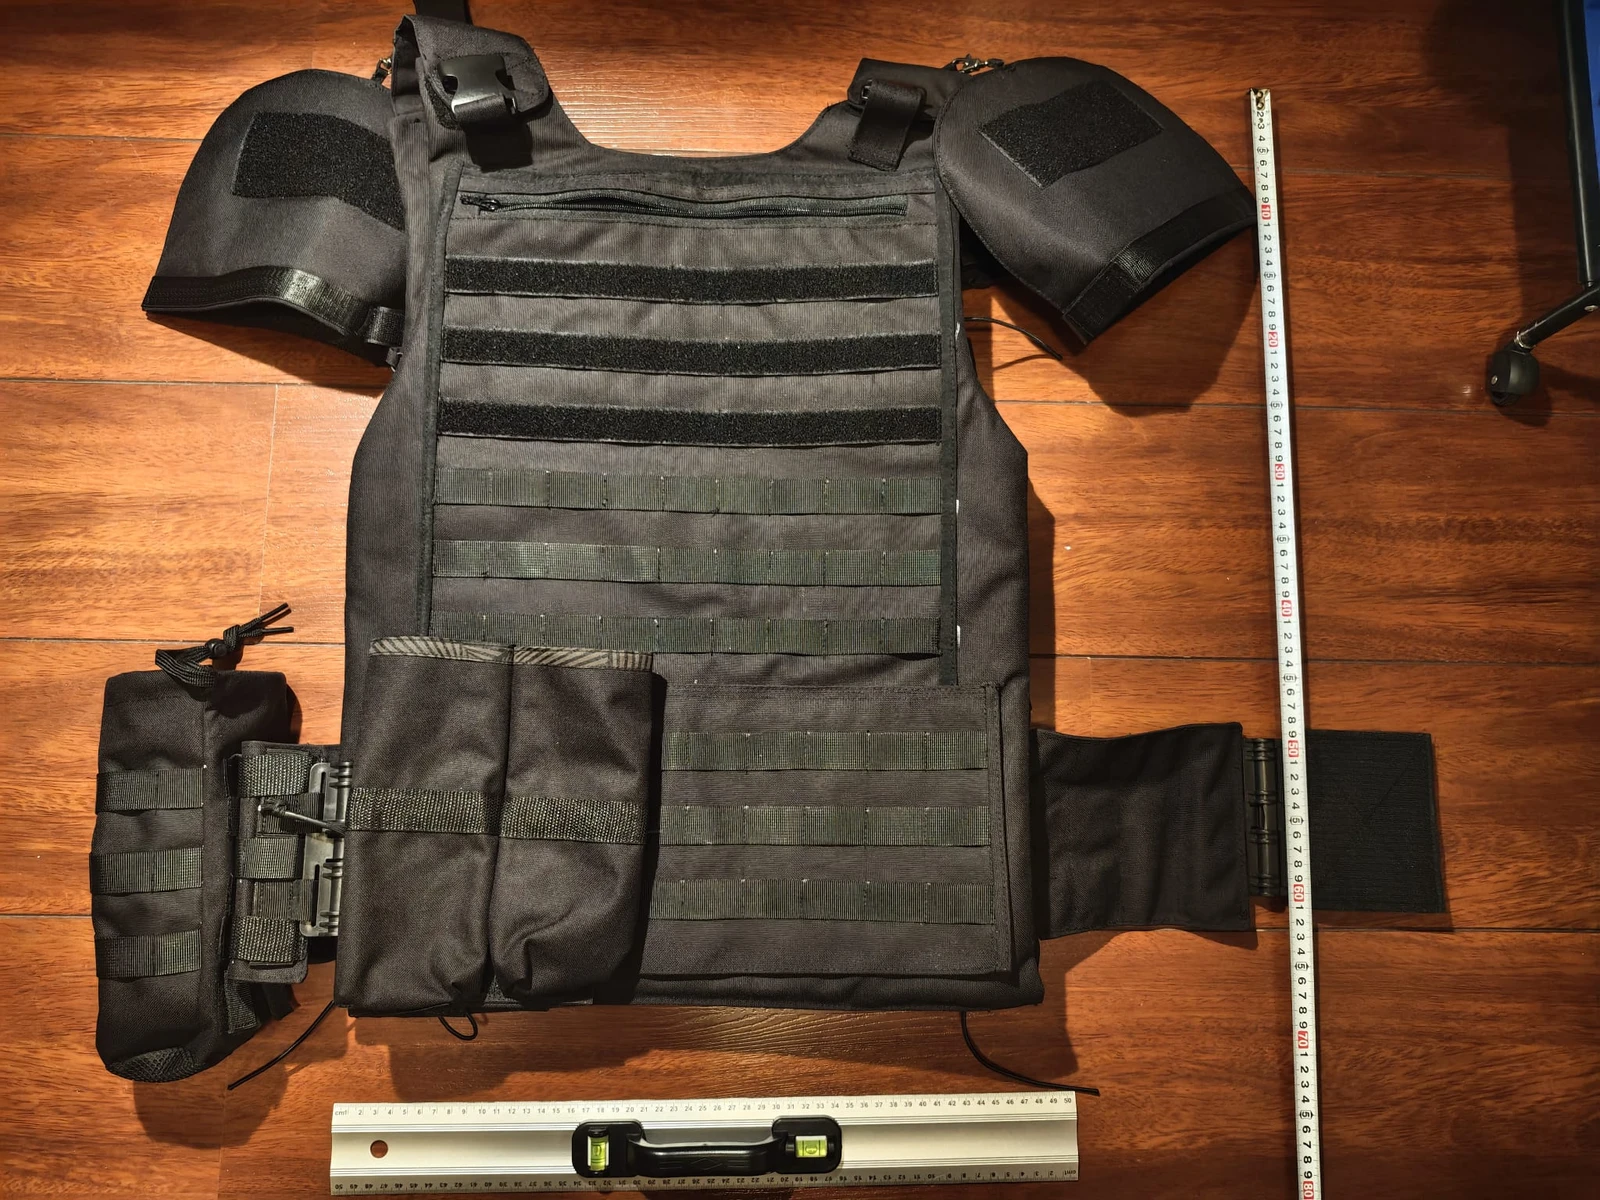
Background
Before this project, I’d looked at plate carriers and tactical vests the way most people do: as finished products that just exist. But I had no idea how they were actually put together. What makes one vest cost $200 and another $2,000? How do you sew through half a dozen layers of nylon and Kevlar on anything less than a factory line? What decisions sit behind the placement of every stitch?
So I decided to build one myself: a real, functional carrier that had to work as a layered protective system. Out of pure curiosity, I wanted to understand the engineering that goes into soft armor, from the material stack-up to the sewing techniques that hold everything together under load.
Requirements
Before I touched any fabric, I wrote down what this thing actually needed to do. I wasn’t designing for a specific military contract: more like “if this were a real product, what would the requirements look like?”
| Requirement | Target | Why It Matters |
|---|---|---|
| Flame resistance | Outer layer self-extinguishing | Welding spatter, hot particles: real industrial hazards |
| Cut resistance | Kevlar layer for blade/shard defense | Metal splinters and tool fragments are surprisingly common |
| Penetration resistance | Hard plate for high-velocity fragments | Fast-moving debris isn’t something fabric alone can stop |
| Impact absorption | 10mm trauma pad | Blunt force behind the plate still needs somewhere to go |
| Modular expandability | Full MOLLE grid integration | A vest that can’t carry pouches is a vest half-finished |
| Adjustable fit | Hook-and-loop at shoulders and waist | Different bodies, different layers underneath: it has to adapt |
| Breathability | 3D mesh air channels | Heat buildup during extended wear is a real problem |
| Total thickness | ~40mm calibrated stack | Protection matters, but if you can’t move it’s useless |
The philosophy I landed on was pretty simple: don’t try to stop everything at once. That’s how you end up with an 80-pound bomb suit that nobody can actually wear for more than ten minutes. Instead, each layer in the stack addresses a specific, realistic threat. Together they cover a practical range of hazards. This is how professional protective equipment actually gets designed: a configurable system.
Choosing Materials: Each Layer Earns Its Place
Every single material in this vest is there for a reason. The stack order matters just as much as the materials themselves: environmental protection on the outside, ballistic and impact protection in the middle, comfort against the body.
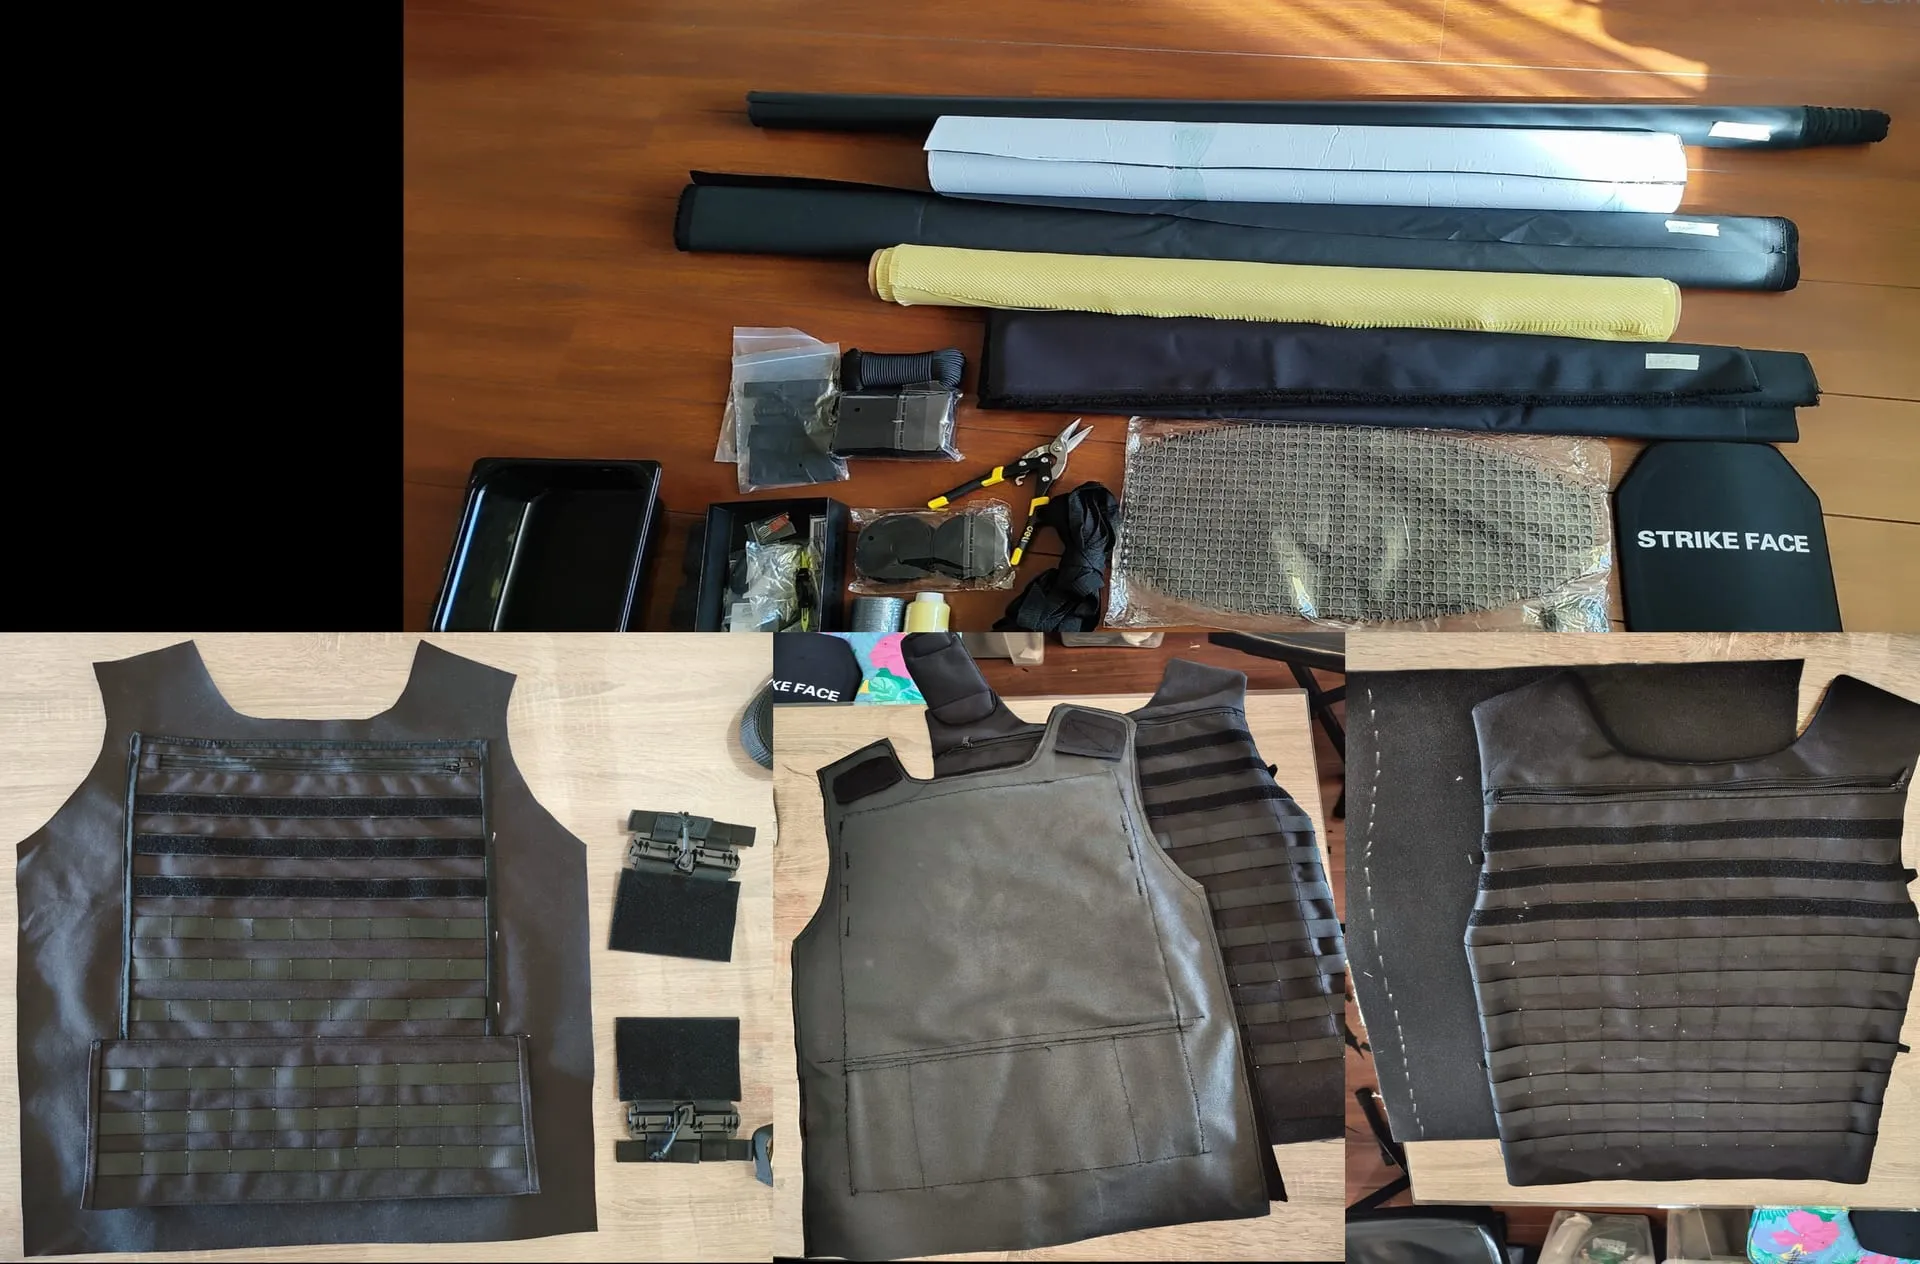
Layer Breakdown (Outside → Inside)
| Layer | Material | Thickness | Function |
|---|---|---|---|
| Outer Carrier | 1000D Oxford Nylon | 0.5–1mm | Flame retardant, waterproof, abrasion resistant, tear resistant. This is the shell that takes all the environmental abuse (UV, moisture, mechanical wear) so the inner layers don’t have to. |
| Soft Protection | Kevlar (Aramid) | 0.3–0.5mm/layer | Scratch, fire, and cut resistant. Handles low-velocity fragments. I placed it inside the outer carrier specifically to shield it from UV exposure, which degrades aramid fibers over time. |
| Hard Protection | Steel Alloy Plate | 8mm | This is the rigid layer. High-velocity fragments, punctures, impacts: anything the soft layers can’t handle alone. It’s the structural backbone of the whole system. |
| Trauma Pad | Ventilated PU Foam | 10mm | Energy absorption and shock dampening. Even if the plate stops a projectile, the blunt force still transfers. This foam layer spreads that impact across a wider surface area to reduce trauma. |
| Inner Carrier | 1000D Oxford Nylon | 0.5–1mm | Same shell fabric as the outside. Encapsulates all the protective layers and gives the ergonomic backing something solid to attach to. |
| Ergonomic Layer | 3D Micro-mesh Air Ducts | n/a | The layer that actually touches the wearer. Ventilation channels create an air gap between body and armor, wicking moisture and reducing the slow heat soak that makes extended wear miserable. |
Building It: Pattern Making, Sewing, and Problem-Solving
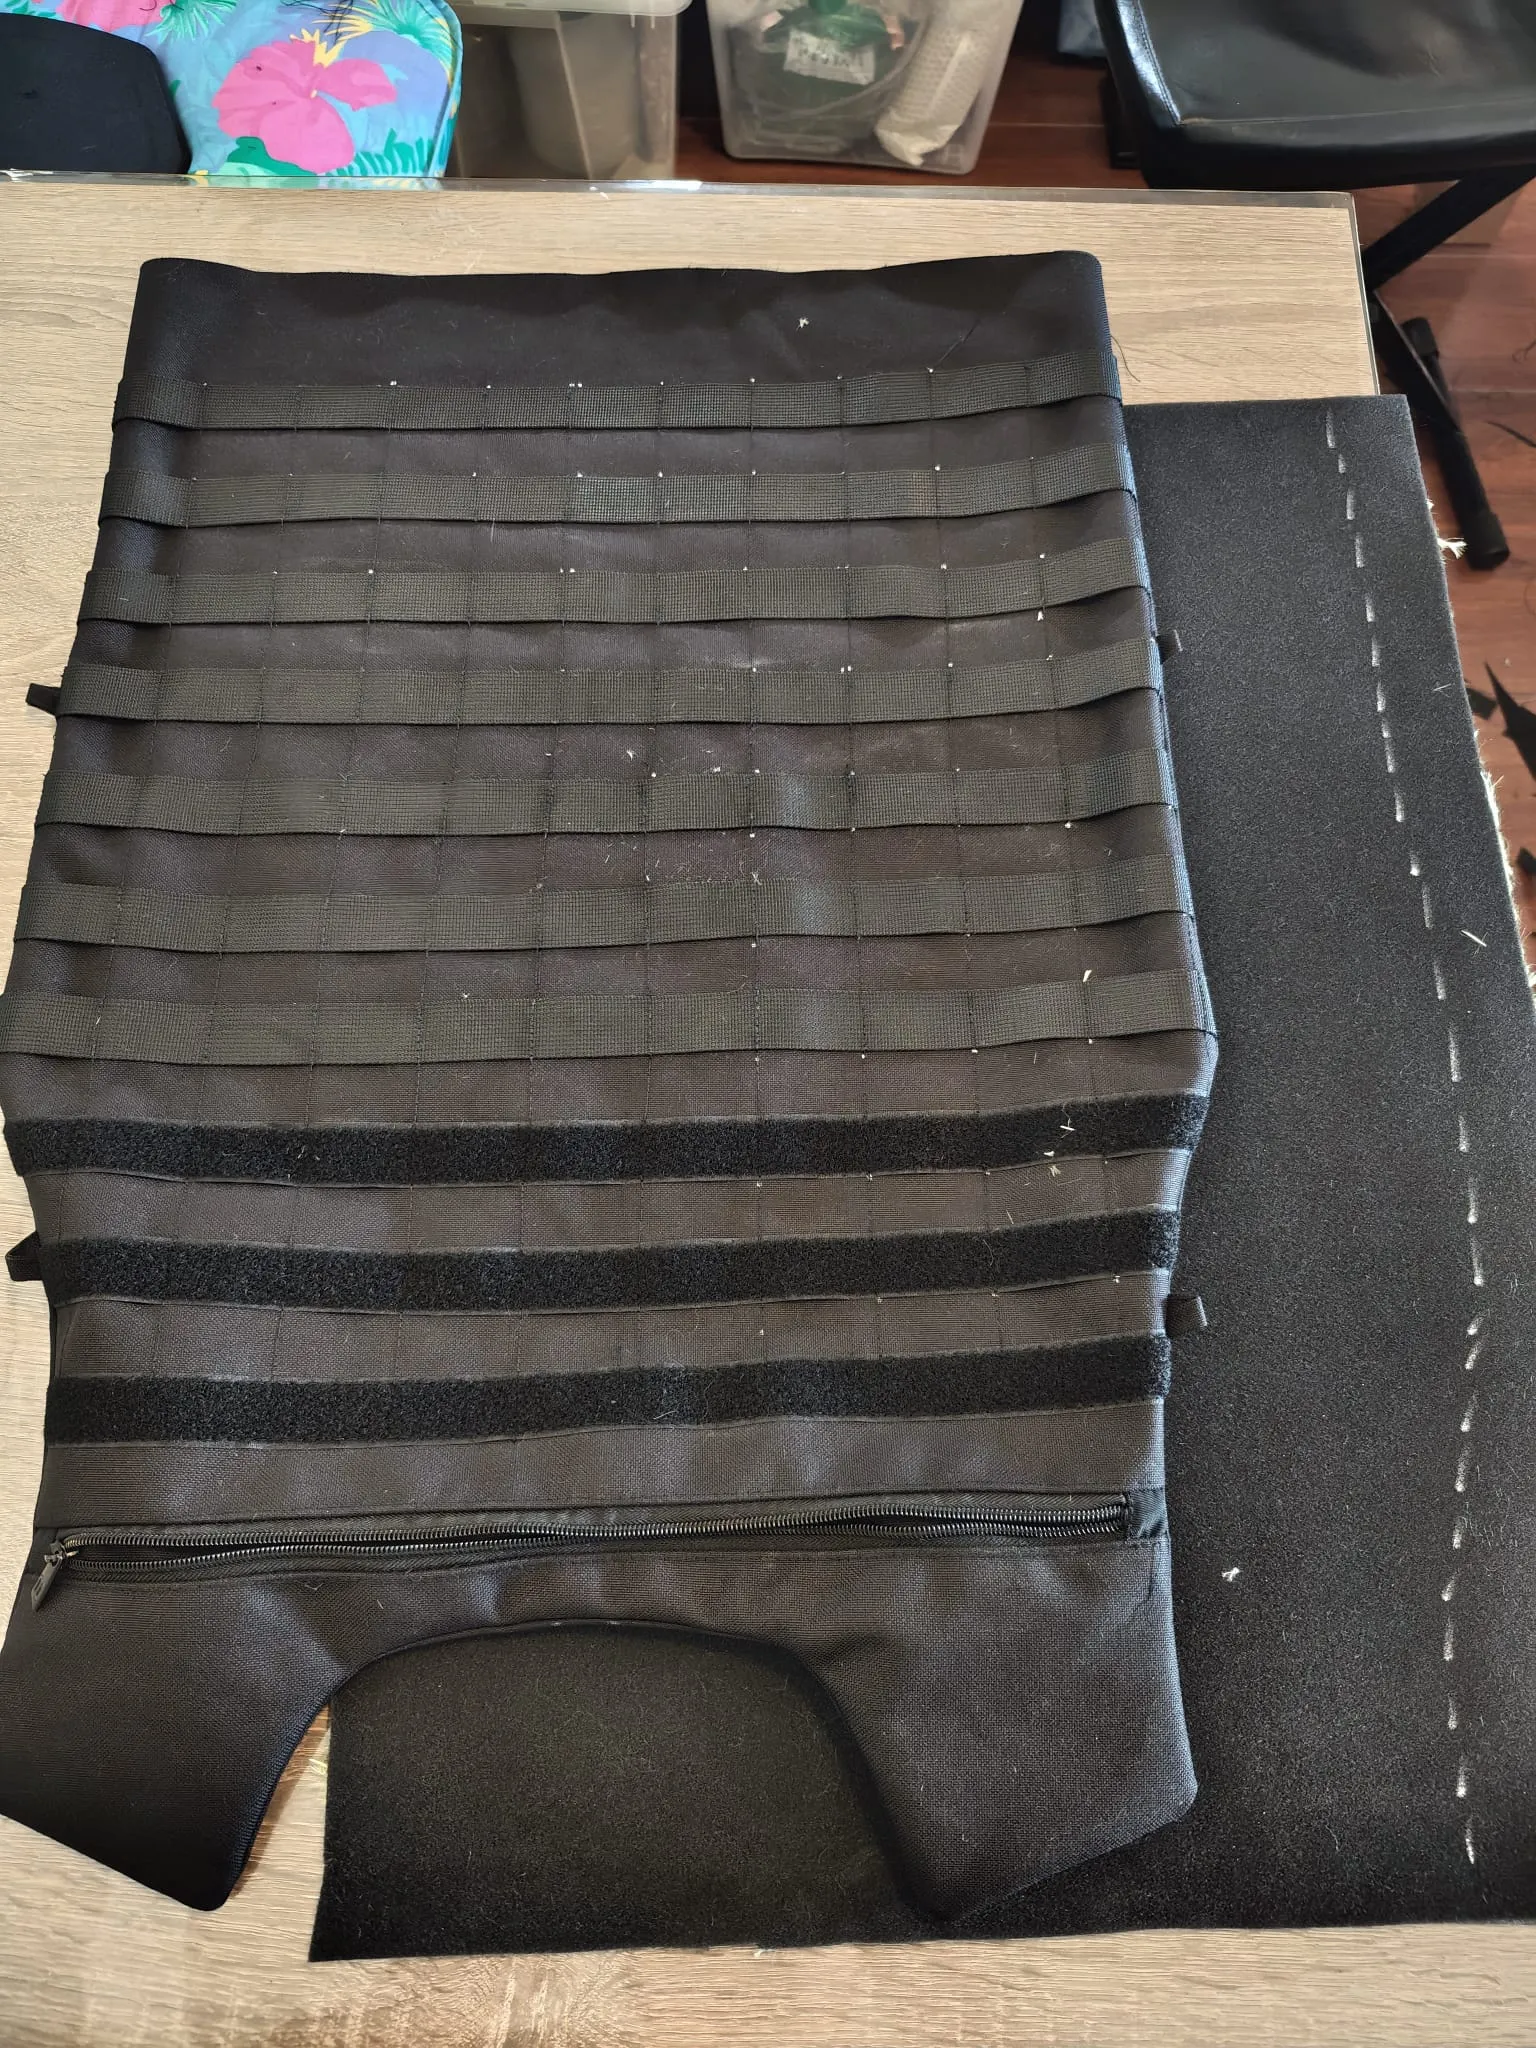
From Paper to Fabric
The workflow was pretty standard for garment prototyping: estimate fabric needs based on body measurements, source the materials, draft paper patterns, transfer to fabric, cut, assemble. Then iterate. Every fitting round revealed something to tweak.
A few things turned up that I had not planned for. 1000D nylon is unforgiving: a standard home sewing machine will laugh at you, and then jam. I needed heavy-duty needles and constantly adjusted thread tension, and for the thickest seam intersections only an industrial walking-foot machine could punch through consistently; even then, going slow was the only option. Kevlar eats scissors for breakfast: you cannot cut aramid fabric with regular shears, because it frays, it slides and it dulls blades almost instantly. I went through a learning curve before accepting that serrated aviation snips were mandatory, and I had to plan seam allowances more generously than I expected because Kevlar edges unravel easily. MOLLE is more than straight-line sewing: the PALS grid looks simple, one-inch spacing and parallel rows of webbing, but every attachment point needs a bartack reinforcement, and if your spacing drifts even a couple of millimeters certain pouches will not fit. It is a standardized interface, and standards do not tolerate slop. Adjustability is its own design problem: hook-and-loop panels at the shoulders and cummerbund let the vest adapt to different body shapes and clothing layers, so you do not have to rebuild the whole thing to adjust the fit, and if you have ever sewn through six layers of nylon you will appreciate that.
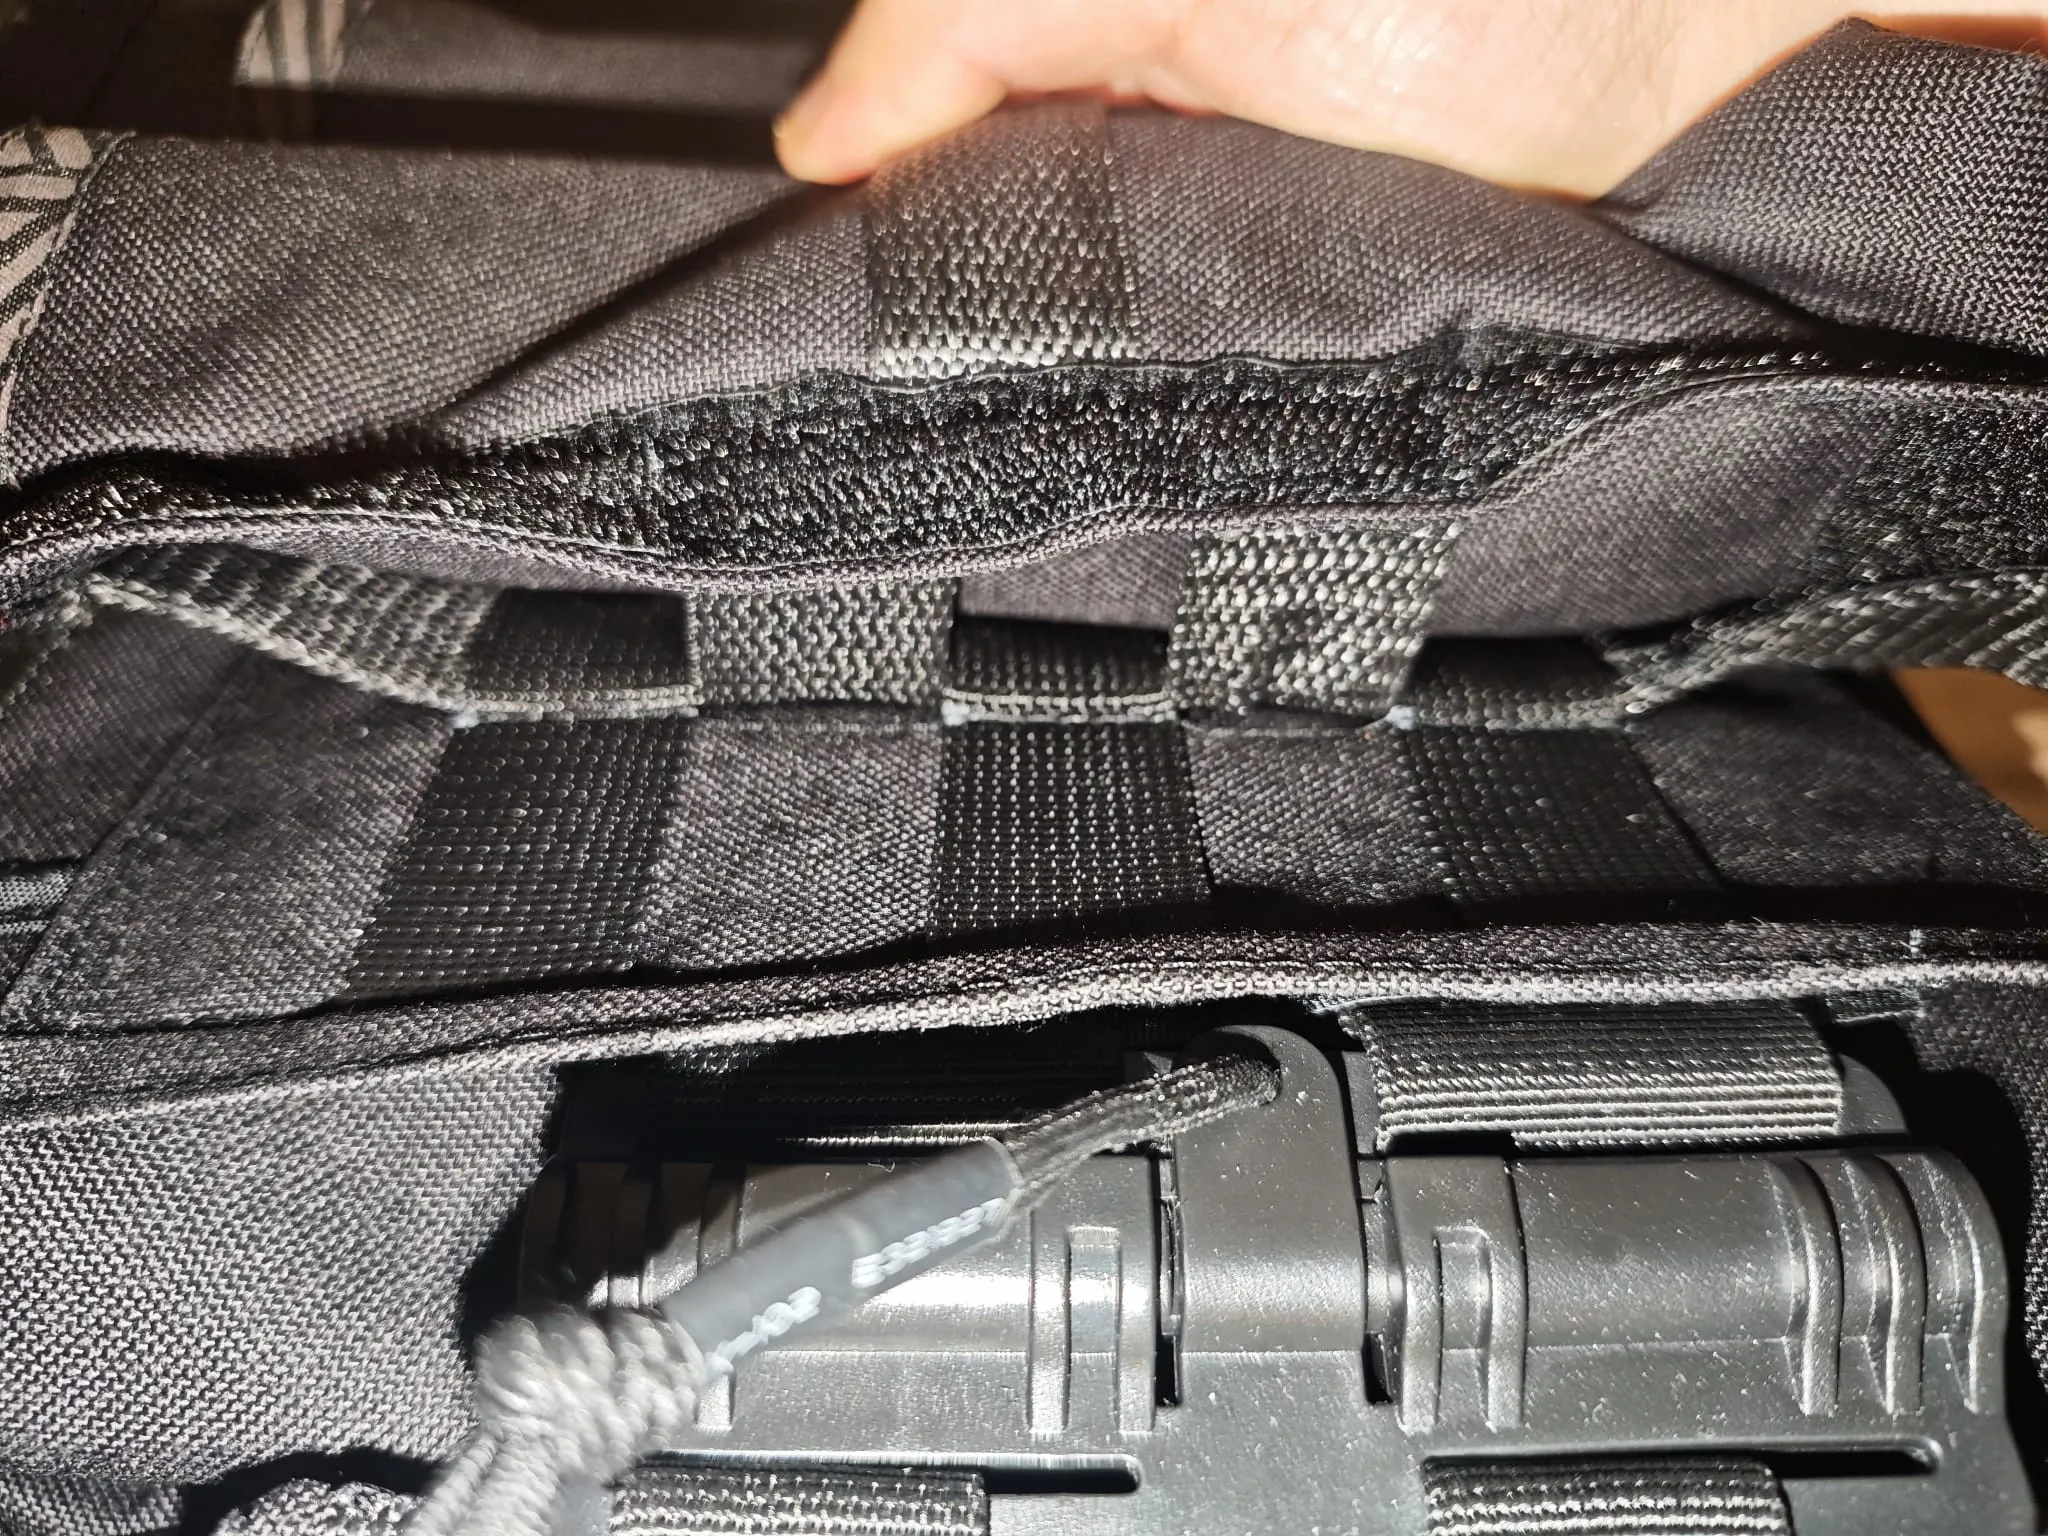
Modularity at Two Scales
I thought about modularity in two directions:
For the wearer, hook-and-loop closures at the shoulders and sides let the vest adapt to your body. For the mission, the MOLLE grid across the front, back and cummerbund lets you attach whatever you need, whether that is pouches, hydration or admin panels, without modifying the carrier itself.
Result
I did as much testing as I could with the equipment I had. If I ever build an optimized version, I would look into approaching a local facility that does this kind of testing:
Fit testing meant multiple wear sessions, checking range of motion, pressure points and how far the adjustments could go; if I couldn’t move comfortably, the ballistic protection didn’t matter. Material compatibility had to be checked in practice, because layering Kevlar against nylon sounds fine in theory but aramid is abrasive stuff and the two can wear on each other during movement. Stitch integrity I tested by yanking on the MOLLE attachment points harder than any pouch ever would: the bartack reinforcements held, and that is where my thread tension experiments paid off. The hard part was the seam intersections, where some join points stacked up 6–8 layers of heavy fabric. I had to grade the seams carefully and swap presser feet to handle the bulk, and that is the kind of thing you don’t appreciate until you’re staring at a sewing machine that physically cannot fit the material under the foot.
Functional Layers Cross-Section
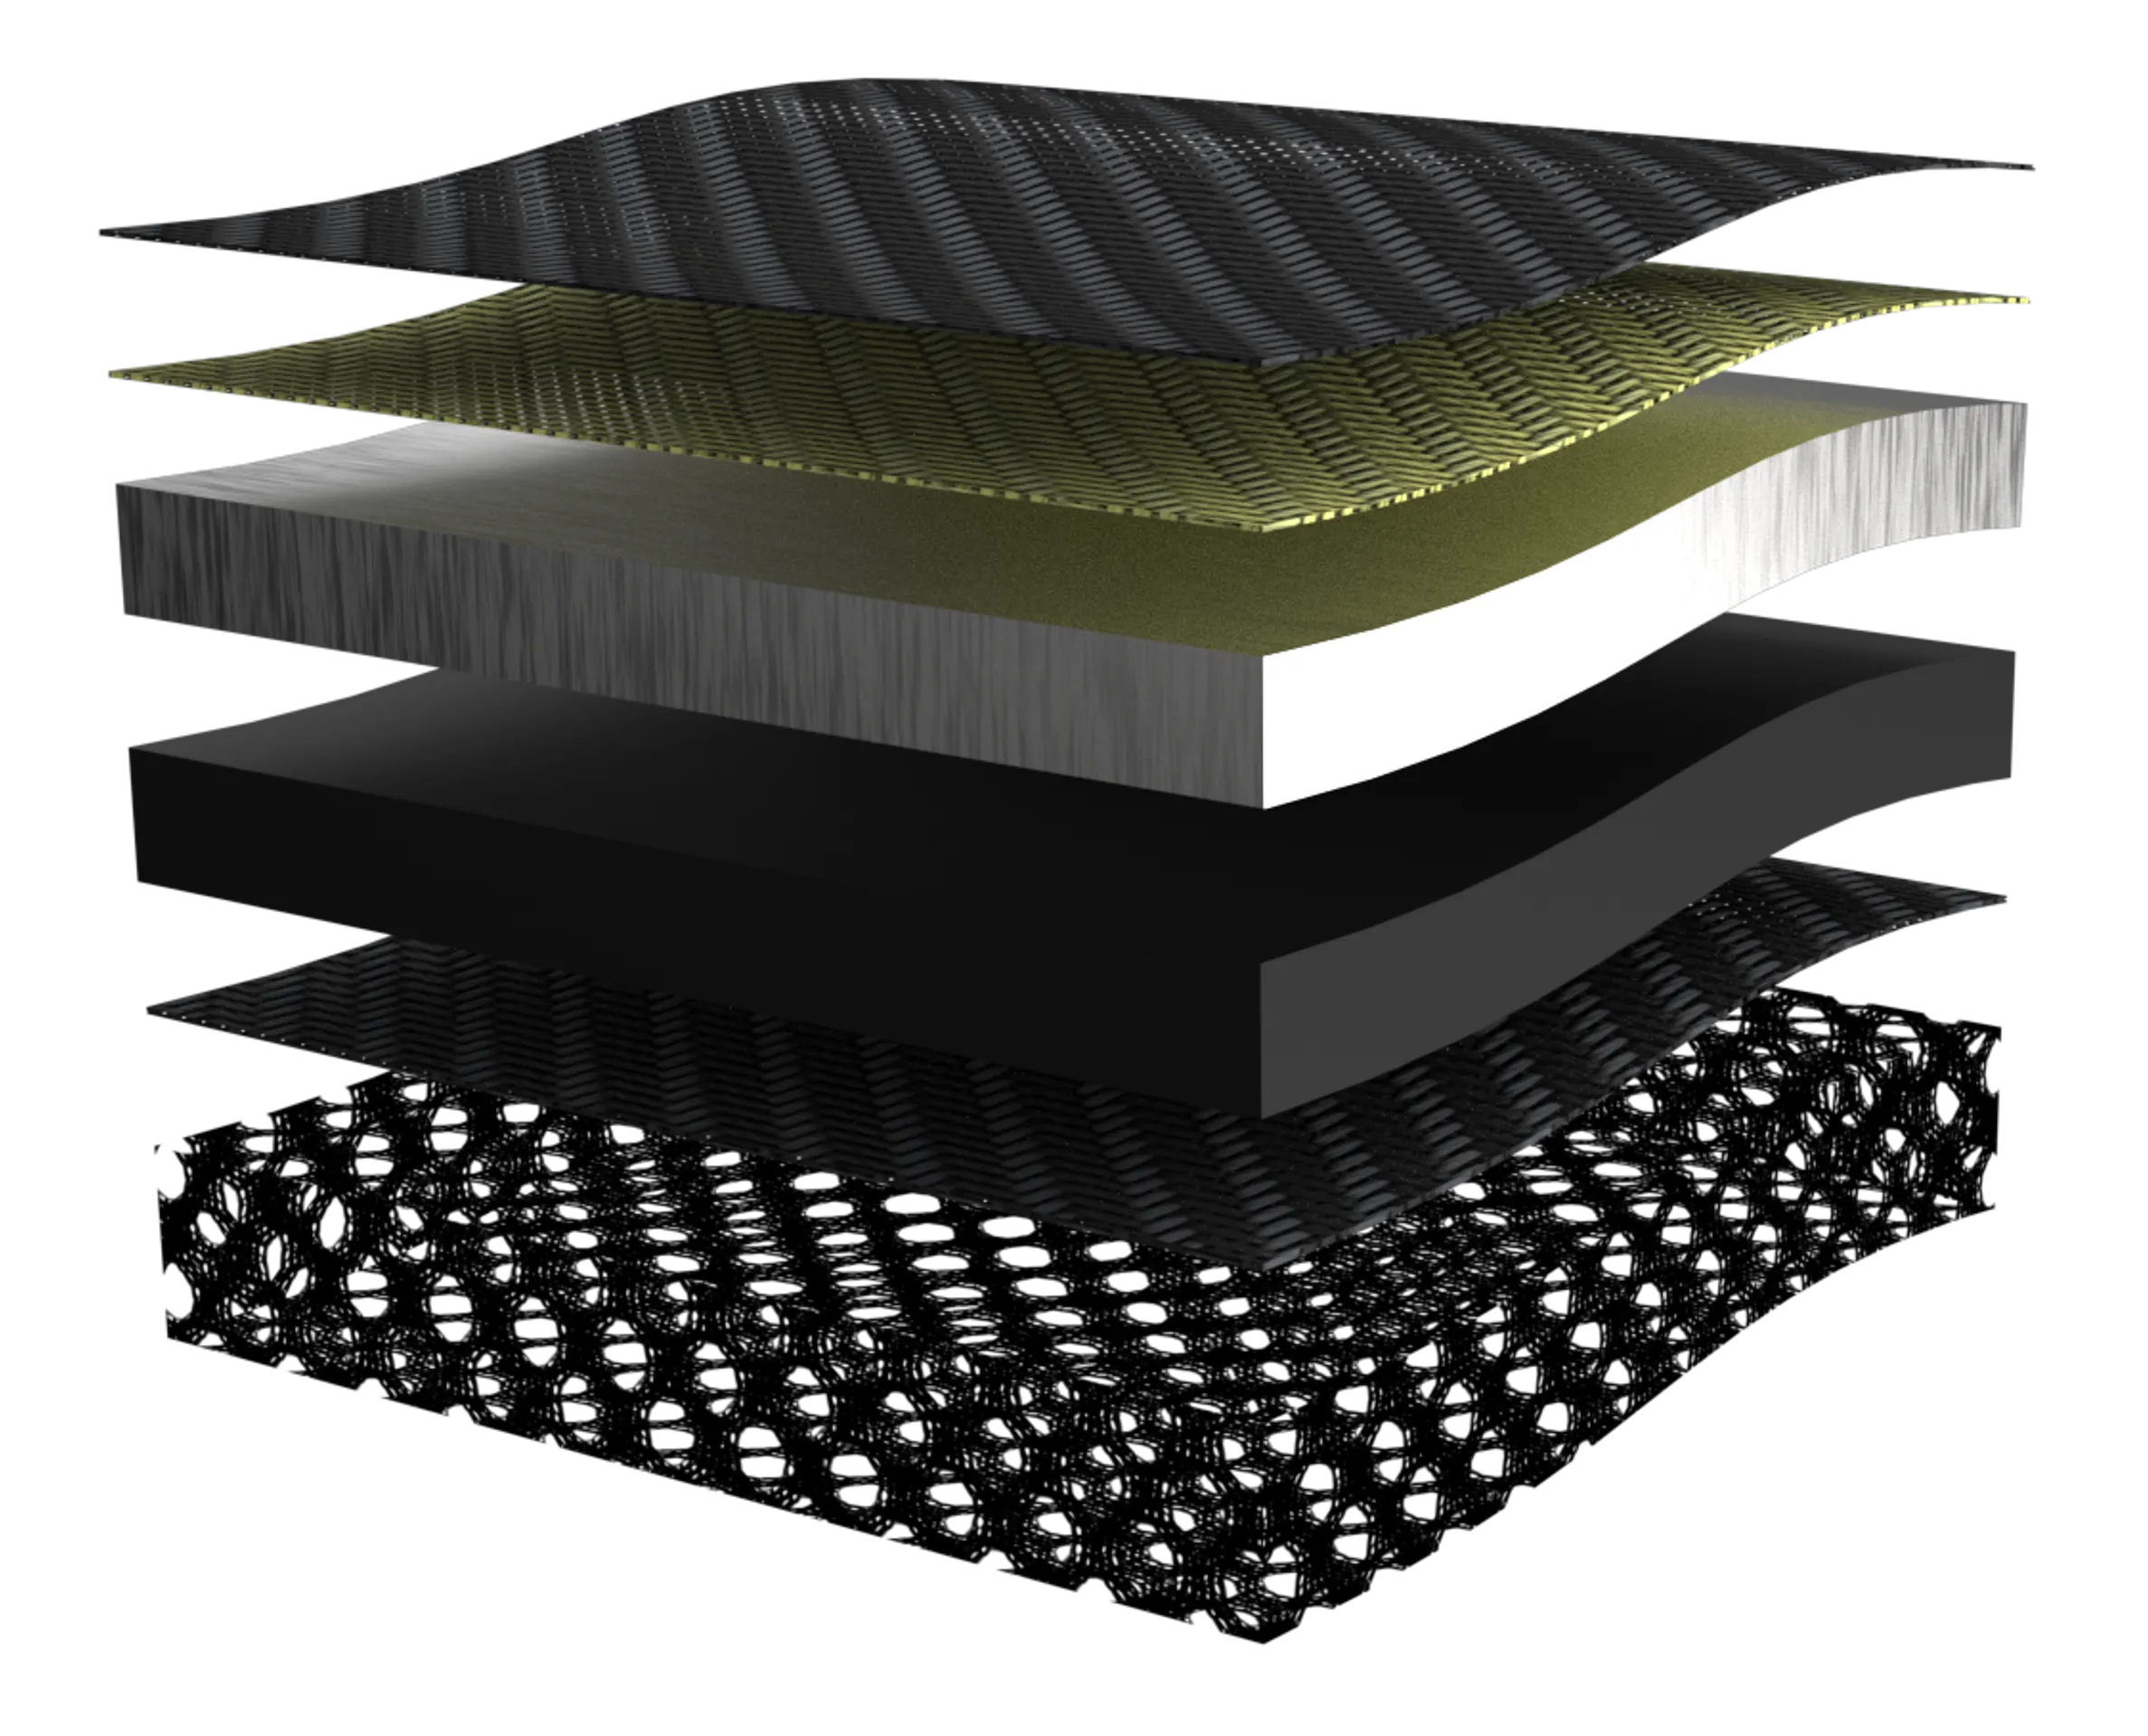
Layer 1: Carrier
1000D Oxford Nylon (0.5–1 mm)
Layer 2: Soft Protection
Kevlar (0.3–0.5 mm per layer)
Layer 3: Hard Protection
Steel Alloy Plate (8 mm)
Layer 4: Trauma Pad
Ventilated PU Foam (10 mm)
Layer 5: Inner Carrier & 3D Cooling Pad
1000D Oxford Nylon + 3D Micro-mesh Air Ducts
What I Learned
I made this to understand a category of objects that I’d only ever seen from the outside.
Garment construction is a whole discipline: pattern drafting, cutting, assembly and finishing add up to a complete production workflow that most industrial designers never touch, and working through it from start to finish gave me respect for every seam I now see on any piece of clothing. Heavy fabrics demand heavy solutions, and 1000D nylon taught me where the line sits between what home equipment can handle and what requires industrial machinery. That line comes fast. Kevlar is its own skill set, because everything about working with aramid, from cutting to handling to seam planning, is different from conventional textiles, and you learn it the hard way by ruining some material first. MOLLE is a case study in interface design: a grid of one-inch spaced webbing sounds trivial, but when dozens of accessory manufacturers depend on that spacing being exact, every single stitch becomes an interface specification, and getting it wrong means nothing fits. And soft goods are still industrial design: choosing materials against performance requirements, designing for manufacturing constraints, thinking about modularity and user fit is the same process as any other product, just with fabric instead of injection-molded plastic.
Before this project, a protective vest was just “heavy clothing” to me. Now I see it as an engineered system: material science, human factors, and manufacturing reality all converging at every single seam. That shift in perspective was the whole point.